
Canola Oil Clarification Decanter Centrifuge for Australia Customer
GN Separation has developed a customized decanter centrifuge solution for a canola oil clarification project in Australia. Designed specifically for edible oil processing, this equipment focuses on efficient solid-liquid separation while paying particular attention to hygienic requirements, operational flexibility, and long-term reliability.
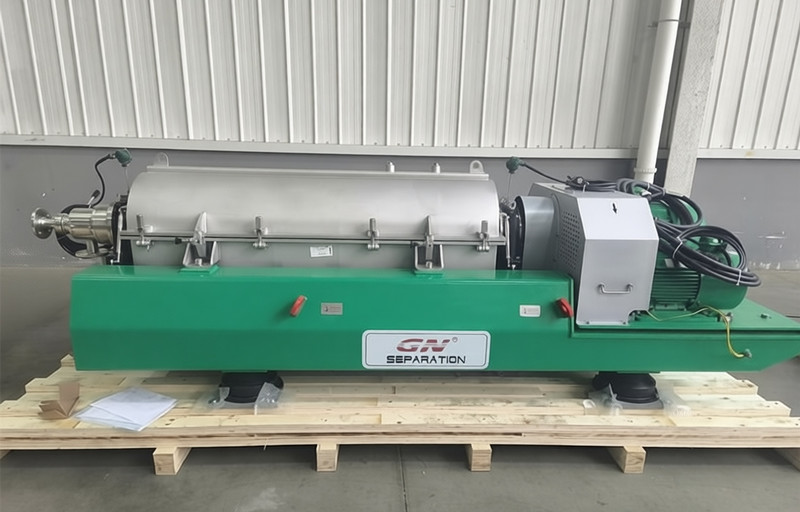
For this Australian customer, GN paid special attention to the internal structure of the centrifuge to meet the specific requirements of edible oil applications. One of the key design features is the polishing treatment applied to the internal screw propeller. The screw surface is carefully polished to achieve a smoother finish, reducing material adhesion and minimizing the possibility of residual materials accumulating inside the equipment. This is particularly important in food-related applications, where material residue left inside the machine may deteriorate over time and potentially affect product hygiene. The improved surface finish also makes internal cleaning easier and helps maintain a cleaner operating environment.
Another important feature is the adoption of a centripetal pump for clarified liquid discharge. Unlike conventional arrangements that may require machine shutdown to adjust the liquid discharge conditions, this design allows operators to flexibly adjust the liquid pool depth without stopping the centrifuge. By changing the liquid pool depth, operators can optimize the separation conditions according to actual feed characteristics and production requirements. This flexibility is valuable when processing materials with varying solid content or other changing process conditions. It also reduces unnecessary interruptions, helping the customer maintain continuous production and improve operational efficiency.
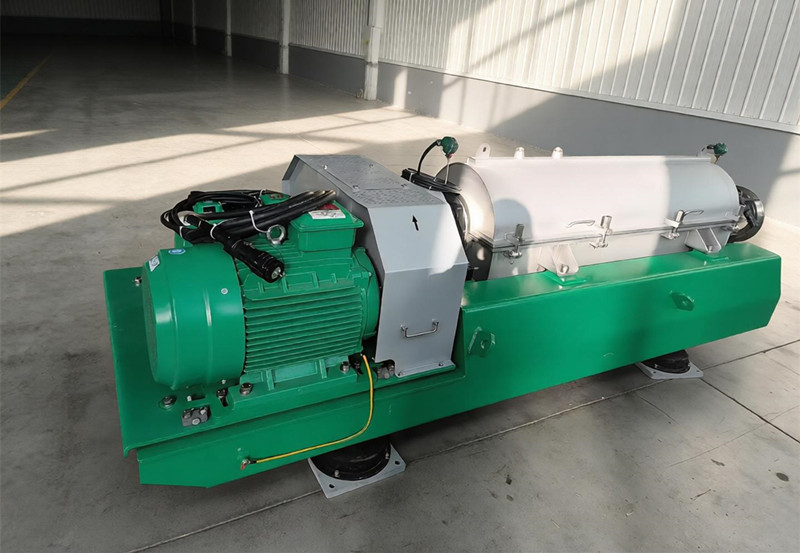
In addition to these customized design features, the decanter centrifuge is engineered to provide stable continuous operation and reliable separation performance. Its compact structure, continuous solids discharge, and adaptable operating parameters make it suitable for integration into industrial edible oil processing lines. The equipment configuration is determined based on the customer's process requirements, with the objective of achieving an effective balance between separation performance, product quality, and operating convenience.
GN Separation has extensive experience in the design and manufacture of industrial decanter centrifuges for applications across food processing, wastewater treatment, oil and gas, and mining industries. Different materials and operating conditions often require different equipment configurations, and GN focuses on adapting its separation technology to the practical needs of each project.
This canola oil clarification project in Australia demonstrates GN's approach to application-specific equipment design. By combining hygienic internal surface treatment with flexible liquid pool adjustment, GN aims to provide the customer with a dependable separation solution that supports efficient processing and consistent product quality.