
5 sets of big bowl decanter centrifuges for overseas tailings slurry separation project
GN Separation has achieved another milestone in the global mining industry with the successful commissioning and stable operation of five GNLW764-VFD big bowl decanter centrifuges at an overseas mining tailings treatment project. Designed to handle demanding slurry separation applications, the equipment demonstrates GN’s capabilities in delivering customized solid-liquid separation solutions for challenging mining environments.
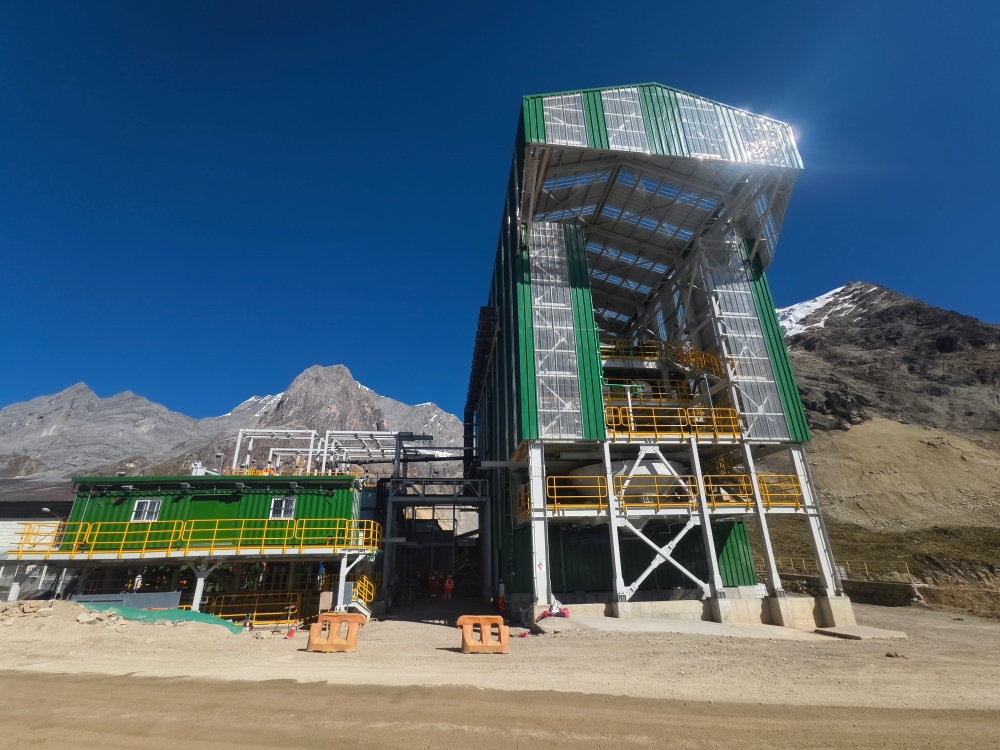
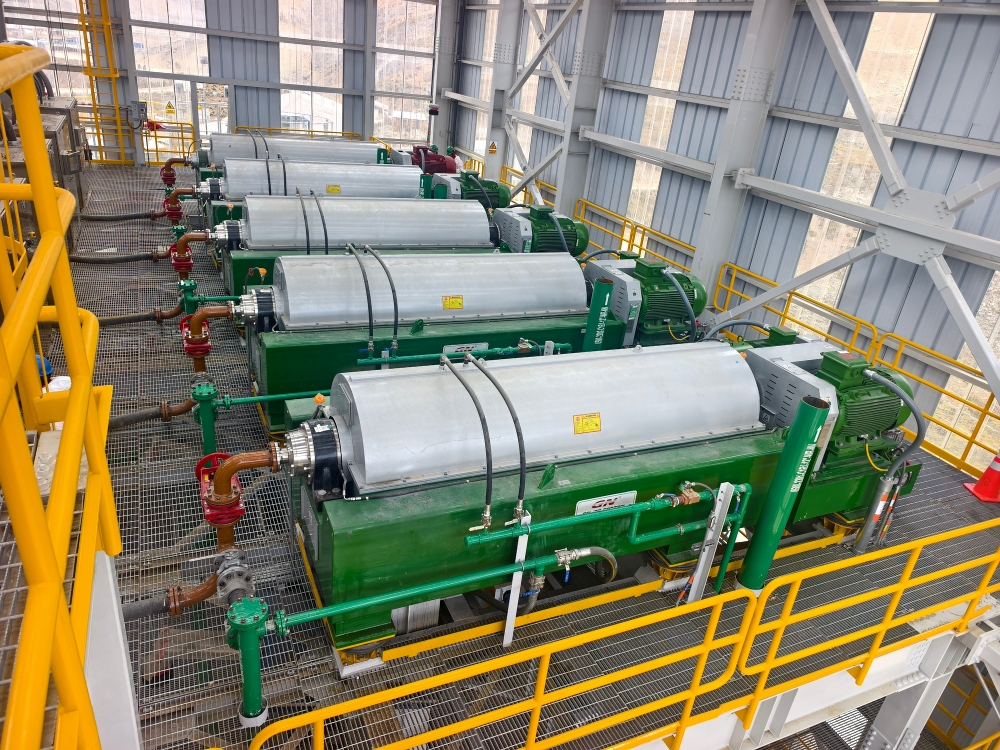 The project was undertaken for a major mining enterprise following a competitive international procurement process. From the outset, the customer required reliable equipment capable of handling large volumes of tailings slurry under demanding operating conditions. Located in a high-altitude mining area approximately 4,500 meters above sea level, the project presented significant challenges for equipment performance, operational stability, and wear resistance.
In addition to the extreme altitude, the application involved high slurry throughput and abrasive mineral particles, which placed considerable demands on the centrifuges’ core components. These conditions required more than a standard equipment configuration. Long-term operational reliability, effective solids separation, and manageable maintenance requirements were essential to the customer’s production objectives.
To meet these requirements, GN Separation developed an equipment configuration tailored to the project's specific operating conditions. The GNLW764-VFD decanter centrifuge features a large 30-inch-diameter bowl and a variable-frequency drive (VFD) control system. The large bowl design provides a suitable configuration for high-capacity tailings treatment, while variable-speed control allows operating parameters to be adjusted to match changing feed conditions and separation requirements.
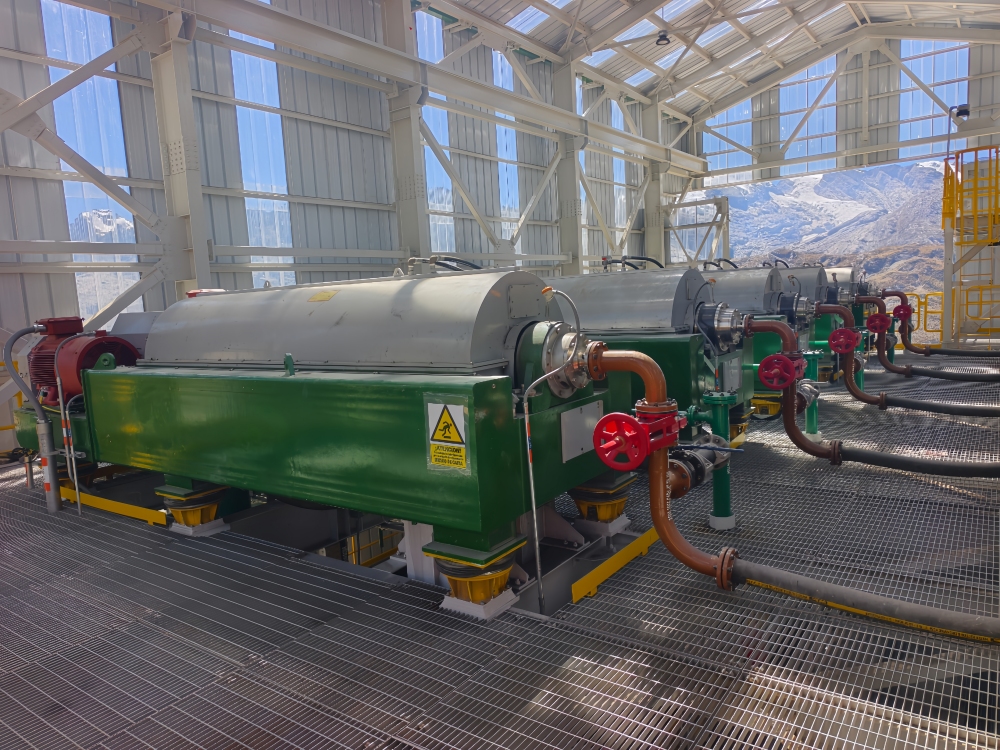
Wear resistance was another important consideration in the equipment design. With abrasive mineral slurry placing continuous stress on key components, GN incorporated wear-resistant design features and optimized material selection for critical wear areas. These measures help improve equipment durability and support continuous operation in demanding mining applications.
Rather than proceeding directly with the full equipment package, the project began with the delivery of one centrifuge for on-site testing. This initial unit allowed the customer to evaluate the equipment under actual site conditions, including separation performance, operational stability, and suitability for long-term production.
Following successful field testing and verification, the customer recognized the equipment’s performance and proceeded with an additional order for four units of the same model. The project ultimately expanded to five GNLW764-VFD decanter centrifuges, demonstrating the value of practical testing and performance validation in building customer confidence.
The complete system includes five big bowl decanter centrifuges, a 6,000-liter automatic chemical dosing unit, and dedicated screw pumps. These components work together to establish an integrated tailings slurry treatment system, supporting continuous feed delivery, chemical conditioning, and solid-liquid separation. The coordinated configuration also helps simplify system operation and provides a practical foundation for efficient plant management.
For mining operators, effective tailings treatment plays an important role in improving process efficiency, managing residual solids, and supporting responsible water and waste management. By separating solids from the liquid phase, decanter centrifuges can help reduce the volume of slurry requiring further handling and facilitate the recovery or reuse of process water, depending on the characteristics of the application and the overall plant design.
The successful commissioning of all five units reflects GN Separation’s ability to respond to demanding customer requirements through equipment customization, engineering support, and field validation. From the initial single-unit trial to the subsequent expansion into a complete five-unit system, the project demonstrates a practical approach to delivering reliable separation equipment for challenging overseas mining operations.
GN Separation continues to develop solid-liquid separation technologies for mining, mineral processing, and industrial wastewater applications. By combining large-capacity decanter centrifuges with application-specific engineering and integrated auxiliary equipment, GN aims to help mining customers improve treatment efficiency, maintain stable operations, and meet evolving environmental management requirements worldwide.